Quality Assured
Muster systems are certified to AS 5062:2022, meeting the compliance requirements of Australia's most demanding industries. Built to the highest standards. Reliable when it matters most.

A correctly designed system is only as good as its installation. MusterFire and its authorised distributor network install fire suppression systems to the exact specification produced by Muster360, on mining equipment, agricultural machinery, transport fleets and industrial plant across Australia and globally.
Find an Authorised InstallerWhen a fire starts on your machine, there is no time to wonder whether your suppression system will work. Muster systems are engineered to remove that doubt entirely. Built to Australian Standards, deployed across mining, agriculture, construction and transport operations worldwide, and backed by a global network of authorised distributors, Muster delivers protection you can count on, every shift, every site, every machine.
Muster systems are certified to AS 5062:2022, meeting the compliance requirements of Australia's most demanding industries. Built to the highest standards. Reliable when it matters most.
From risk assessment and system design through to installation, maintenance and training, our expert distributor network provides end-to-end support. Rapid, reliable, and always compliant.
Continuously evolving to meet the demands of modern heavy industry, from autonomous vehicles to electric fleets.
Our suppression agents are fluorine-free and environmentally responsible. Muster systems are designed with ecological impact in mind, meeting global environmental protection standards without compromising on performance.
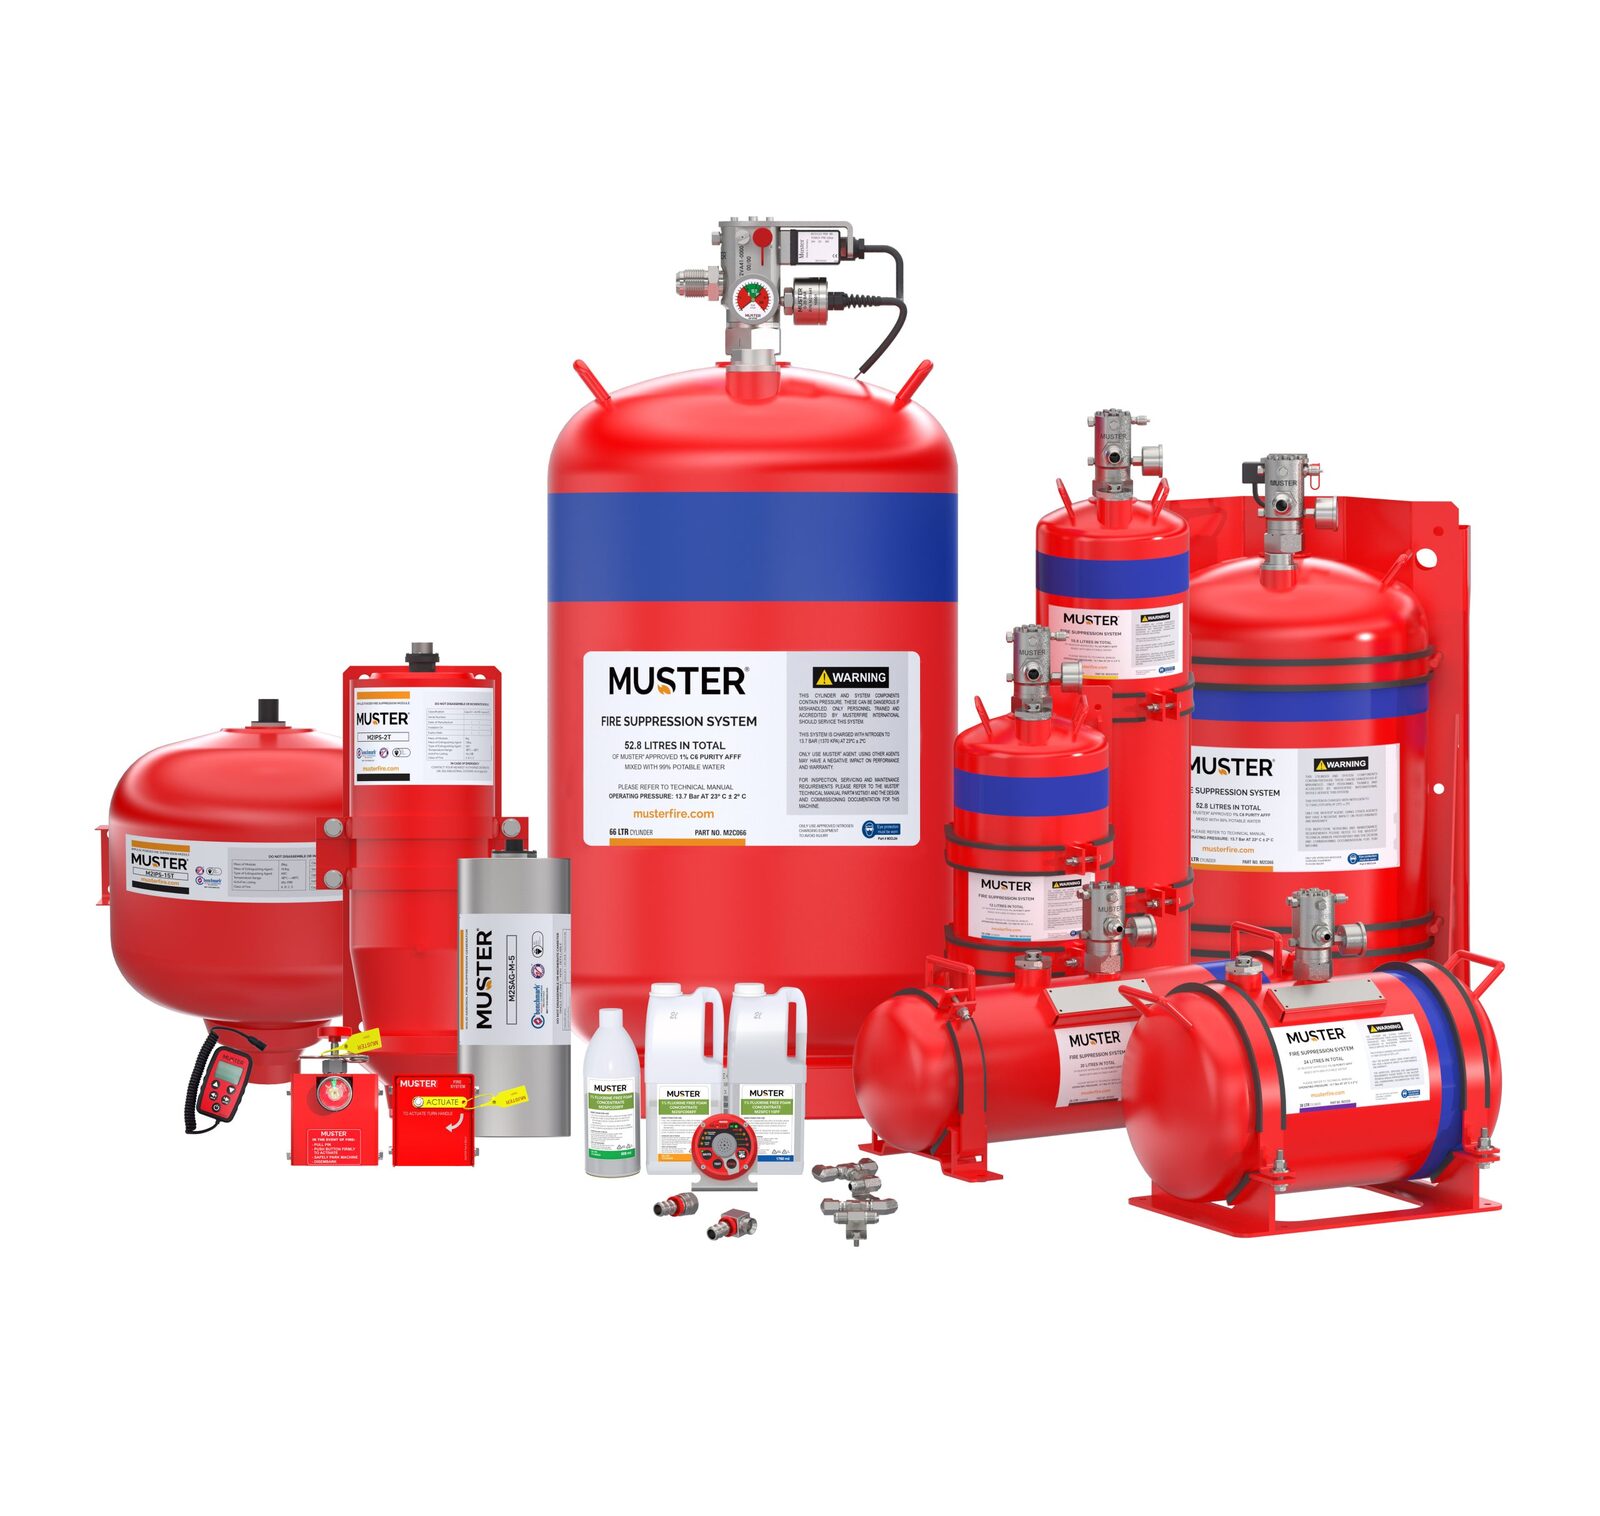
Most widely installed Muster product. Fluorine-free foam (F3) with stainless steel cylinders, valve assemblies and precision nozzles installed to Muster360 spec.
Full 360° valve orientation for easy access. Pre-engineered kits with modular stainless components for rapid installation and re-commissioning.
No pipework, no plumbing. SAG canisters mount directly to enclosed compartments. Up to 8 units per installation via the Integration Module.
Compact self-generating unit installed at primary fire zones. Available with push-button or lever remote actuators in stainless steel.
ABE powder, CO2, foam. Installed with vehicle brackets and signage as the mandatory supplementary layer alongside every automatic system.
Commissioning is completed using Muster360 documentation. Post install service checklists provided tailored to the machine.
Cloud based commissioningFire suppression system installation on heavy equipment is not a general mechanical task. Nozzle placement that deviates even slightly from the design can leave critical protection zones exposed. Cable routing that does not account for vibration and heat causes premature failure. MusterFire's authorised installers are trained on MusterFire-specific product knowledge, commissioning procedures and compliance requirements.
Installer reviews Muster360 design documentation and confirms all components are on-hand and the machine is prepared.
Cylinders, actuation valves and detector heads are mounted to specified locations using MusterFire-certified brackets.
Discharge nozzles are positioned exactly as per the layout diagram, targeting each identified fire risk zone.
Detection is routed carefully along risk areas, protected against heat, abrasion and vibration for immediate response.
System is operated, detection circuits tested, alarm panel function verified and discharge performance confirmed before machine handover.
Signed commissioning certificate, as-installed diagram and maintenance schedule provided to the machine owner.
Connect with your nearest MusterFire authorised distributor for an installation quote based on your Muster360 system design.
MusterFire systems must be installed by an authorised MusterFire distributor trained on product specifications, Muster360 design documentation and AS 5062 commissioning requirements.
A single-zone installation on a small machine can be completed in half a day. A multi-zone system on a large mining excavator typically takes one to two full days.
Yes. The machine must be clean, cool and de-energised. MusterFire works with operators to schedule installation during planned maintenance windows to minimise operational disruption.
A signed commissioning certificate, as-installed system diagram, maintenance schedule and a copy of the Muster360 design documentation. Required for site safety file compliance and insurer verification.
Yes. Retrofit installation is standard for MusterFire. The Muster360 design process accounts for existing machine geometry, access constraints and any pre-existing fire protection hardware.
MusterFire products carry product warranty terms. Authorised installers provide workmanship warranties on their installation services.
Installation must be carried out by MusterFire authorised personnel to maintain compliance certification. If your workshop team wants to participate, enquire about joining the authorised distributor program.
MusterFire systems are designed to install without permanently modifying the machine's primary structure. Mounting is via bolt-on brackets and clamped cable routing.
Use the MusterFire distributor locator on this website or contact MusterFire directly. Our network covers major mining, agricultural and industrial regions across Australia and internationally.
It is replaced with a genuine MusterFire part of the correct specification. No substitutions outside the certified bill of materials are made without MusterFire engineering approval.