

Mining
Fire Suppression Systems for Mining Equipment
Muster System RangeVersatile Fire Suppression for Every Mining Challenge
Mining environments present a high risk of fire due to heavy machinery, combustible materials, and demanding operating conditions.
Certified to AS 5062:2022, Muster Fire Suppression Systems are independently verified to meet Australia's stringent requirements for mobile and transportable equipment, delivering proven protection for mining applications.
- Flexible heat detection capabilities enabling immediate activation upon detection of fire ensuring minimal damage to assets and personnel
- Multiple fire suppression agents for various fire classes ensuring comprehensive coverage against different fire types
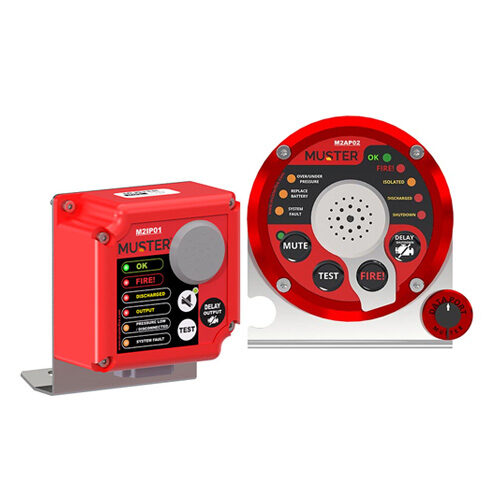
- Advanced integrated control system that incorporates control, monitoring and activation of the Muster fire suppression system.
- Reduce the risk of inury or fatality by controlling fires before they can escalate.
Fire Protection Solutions
- Foam Systems
- IPS
- SAG System
Why Muster
Muster offers full-service fire suppression solutions, from risk assessment and design to purchase, installation, maintenance training, and ongoing monitoring.

How it works

Diagnostic Module
Remote Activation Device
Remote Actuators
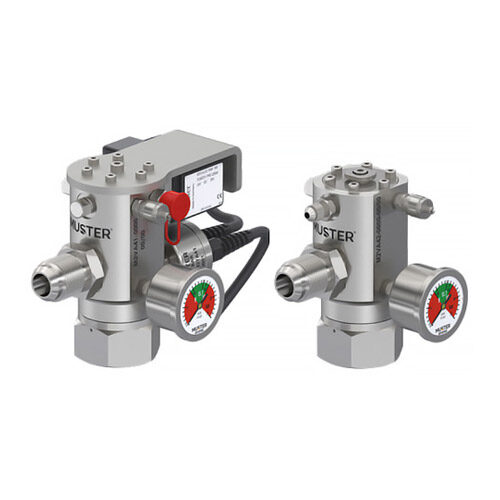
Cylinder Valves
Ready to Get Started?
Muster Automatic Detection Systems
Muster offers two different fire detection methods: Linear Heat Detection (LHD) and Loss of Pressure (LOP). LHD is an electrically controlled system, while LOP operates mechanically. Both systems are designed to provide early fire detection followed by activation of the fire suppression system.

Linear Heat Detection (LHD)
- If fire is detected, the control panel receives a signal, automatically entering FIRE mode.
- Once activated, the control panel sounds an audible alarm, initiates the shutdown sequence and triggers the cylinder valve to discharge the foam to the fire.
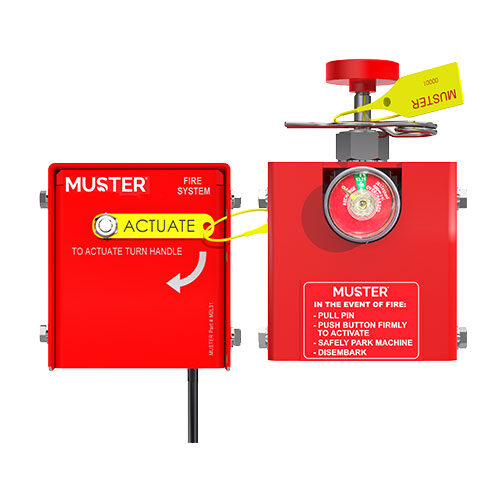
- Fire mode can also be activated by using the remote actuator.

Loss of Pressure (LOP) Detection
- If fire is detected the pressurised sensor tube will rupture, releasing inert gas.
- The release of gas triggers the cylinder valve to discharge foam to the fire.
- The cylinder valve can also be manually triggered with the remote actuator.
Related Systems

Foam Based System
Foam-based fire suppression systems are the most suitable solution for the protection of mobile machinery where liquid hydrocarbon fuels pose a high fire risk. (Read More)

Aerosol System
Self-generating, environmentally responsible, fire suppression system that provides immediate protection to confined spaces. Easy to install with long operational life. (Read More)

Impulse Powder System
Self generating, rapid discharge dry chemical powder in a non-pressurised canister. Compact in design for protected enclosures. Mount directly within the risk area. (Read More)
Protect Your Future
Solutions for Autonomos Vehicles
In the autonomous mining landscape, machines operate tirelessly without human oversight. Muster's automatic fire suppression system ensures rapid fire response and fault detection, swiftly suppressing fires, alerting your control center, offering peace of mind and asset protection.
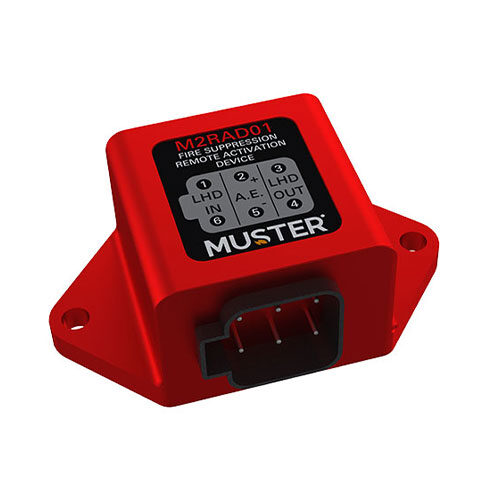
The Muster remote activation device designed for autonomous vehicles allows for the remote activation of fire suppression systems from a distance. Revolutionising fire incident management in autonomous vehicles.
The Scale of Fire Risk in Australian Mining Operations
According to NSW Resources Regulator data, fire incidents on mobile plant machinery continue to be a significant risk across Australian mine sites, with hundreds of incidents reported across surface and underground operations in recent reporting periods. The consequences extend far beyond the machine: production downtime, site evacuation, emergency response, equipment replacement, and regulatory investigation can collectively represent losses orders of magnitude greater than the machine's value.
Most Common Ignition Causes
Turbocharger oil seal failure; fuel or hydraulic hose chafing on hot surfaces; electrical arcing; brake heat buildup on haul truck descents; grease accumulation near exhaust components.
Highest Risk Machine Types
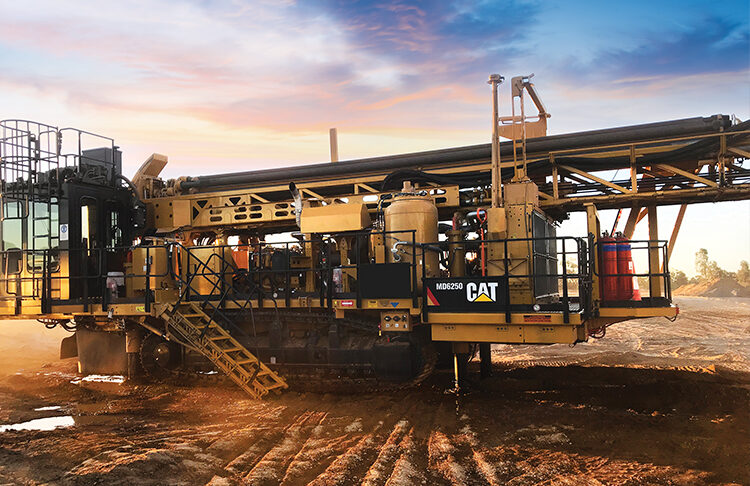
Mining excavators and haul trucks account for the highest proportion of fire incidents due to their size, fuel volume, and hydraulic system complexity.
AS 5062:2022 Compliance
The current Australian Standard for fire protection of mobile and transportable equipment. Required by most major Australian mining operators for all mobile plant as a condition of site access.
Muster in Mining
MusterFire systems are trusted by major mining companies across Australia, with distributor partners providing front-line support across NSW, Queensland, and Western Australia.
Fire Suppression for Mining Equipment by Machine Type
Mining Excavators
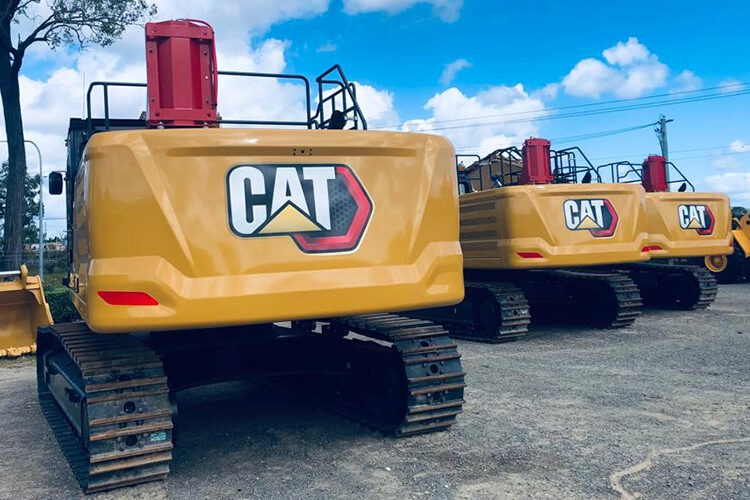
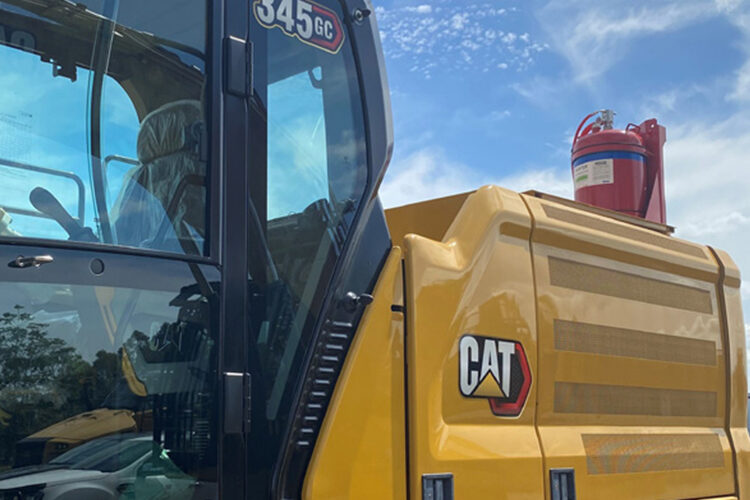
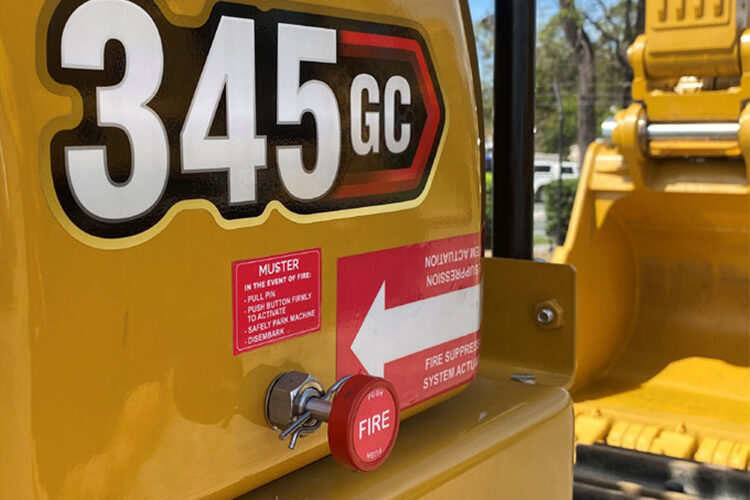
Multi-zone coverage required: foam for the engine bay and fuel/hydraulic areas, SAG for alternator and electrical bays. Three CAT 345 GC excavators were fitted with Muster foam systems and commissioned prior to export from Brisbane port.
Haul Trucks
Surface haul trucks carry large fuel volumes and operate in high-temperature environments. Foam systems cover the engine bay and wheel motor areas, with remote actuators for operator-initiated discharge from the cab.
Graders and Dozers
Foam or misting systems sized to the engine bay configuration. Muster360 system design table ensures correct cylinder sizing and nozzle placement for each machine make and model.
Underground Loaders
Underground mobile equipment requires systems meeting AS 5062:2022 underground requirements, with robust detection and reliable activation in challenging confined conditions.
Technology That Keeps Pace with Modern Mining Operations
Muster360
Access commissioning documentation and manage maintenance scheduling across multiple machines and mine sites from a single platform.
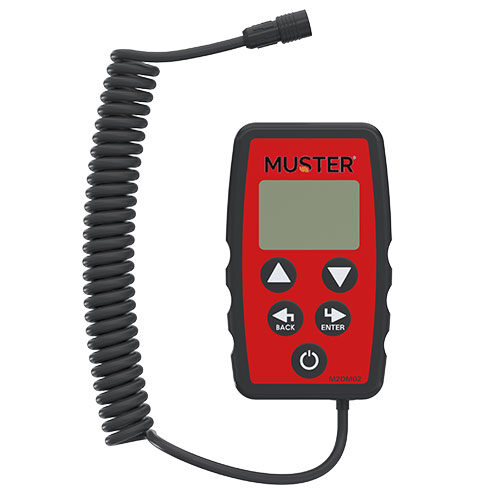
Diagnostics Module
Real-time monitoring of alarm parameters, system pressure, battery status, and software updates. Second-generation design built for harsh mine site conditions.
Remote Activation
The Muster Remote Activation Device allows remote suppression activation without an operator on the machine — critical for autonomous mining equipment fleets.
Fleet Management
Centralised compliance documentation and maintenance tracking across every fitted machine in the fleet.

AS 5062:2022 Compliance for Australian Mine Sites
AS 5062:2022 (Fire Protection of Mobile and Transportable Equipment) is the current Australian Standard mandated by most major mining operators and required under state mining safety regulations for new and existing mobile plant. The standard specifies requirements for system design, detection method, alarm panel functionality, commissioning documentation, and maintenance intervals.
All Muster foam-based and misting systems are certified to AS 5062:2022. Commissioning documentation generated through Muster360 for each installation confirms compliance and provides the documentation required for site safety management systems, WHS files, and insurance records.
How to Buy
MFI partners with authorised distributors to offer you localised sales, installation and service of our products. Find a local distributor, contact your local MFI sales representative or our friendly customer services team.
FAQs
Is fire suppression mandatory for mining equipment in Australia?
Yes, for most mobile plant on Australian mine sites. AS 5062:2022 is the standard mandated by major mine operators as a condition of site access, and state mining safety legislation specifies fire protection requirements for mobile plant.
Which Muster system is best for mining excavators?
Large mining excavators typically require a multi-zone approach: a foam-based system for the engine bay and fuel/hydraulic areas, and SAG units for enclosed electrical and alternator bays. The correct system is determined through a risk assessment using Muster360 by your authorised distributor.
Can Muster systems be used on autonomous mining vehicles?
Yes. Muster systems are designed for both manned and autonomous operations. The Remote Activation Device allows fire suppression to be triggered from a safe distance, and the system activates fully automatically on fire detection without any operator present.
What does AS 5062:2022 require for mining mobile plant?
AS 5062:2022 specifies requirements including: fire risk assessment basis for system design, detection method selection, alarm panel functionality, agent selection and nozzle placement, commissioning documentation, and maintenance intervals.
What is the difference between LHD and LOP in mining applications?
LHD runs a heat-sensitive cable along the risk zone and activates the alarm panel electronically on detecting heat at any point. LOP uses pressurised tubing that ruptures mechanically at the point of flame contact, triggering discharge without electrical activation.
How is a Muster system maintained on a mine site?
Muster systems are maintained by authorised distributors on a service schedule confirmed during commissioning. The alarm panel diagnostics module enables real-time monitoring of system pressure and battery status. Muster360 tracks commissioning records across the fleet.
Can Muster systems be managed across a large mining fleet?
Yes. Muster360 provides centralised compliance documentation management across multiple machines and mine sites.
Which mining distributors supply and install Muster systems in Australia?
Muster systems are supplied and installed by a network of authorised distributors including Paull and Warner Resources (PWR) and Amet Industries. Use the Find Distributor tool on musterfire.com to locate your nearest distributor.
What happens when a Muster system activates on a mine site?
The alarm panel enters FIRE mode, sounds an audible alarm, initiates machine shutdown, and triggers discharge. The event is logged in Muster360. Following discharge, an authorised technician must inspect the machine, recharge the system, and complete an incident report before the machine returns to service.
Is fire suppression required for underground mining equipment?
Yes. Underground mining equipment has specific and stringent fire protection requirements under Australian mining safety regulations due to the confined environment, limited egress, and restricted emergency service access.